
Views: 0 Author: Site Editor Publish Time: 2026-10-05 Origin: Site


Article Intro: A brand mark can be printed into a jewelry pack, or it can arrive as a separate component and be bonded to one. The second route is what private-label programmes and small brands use most: no printing plate is needed, and the mark can go on after the pack is made. It is also where failures are least understood. A mark lifts at one corner, releases cleanly, or takes the board with it, and nobody can say which variable decided it. Two published peel studies can.
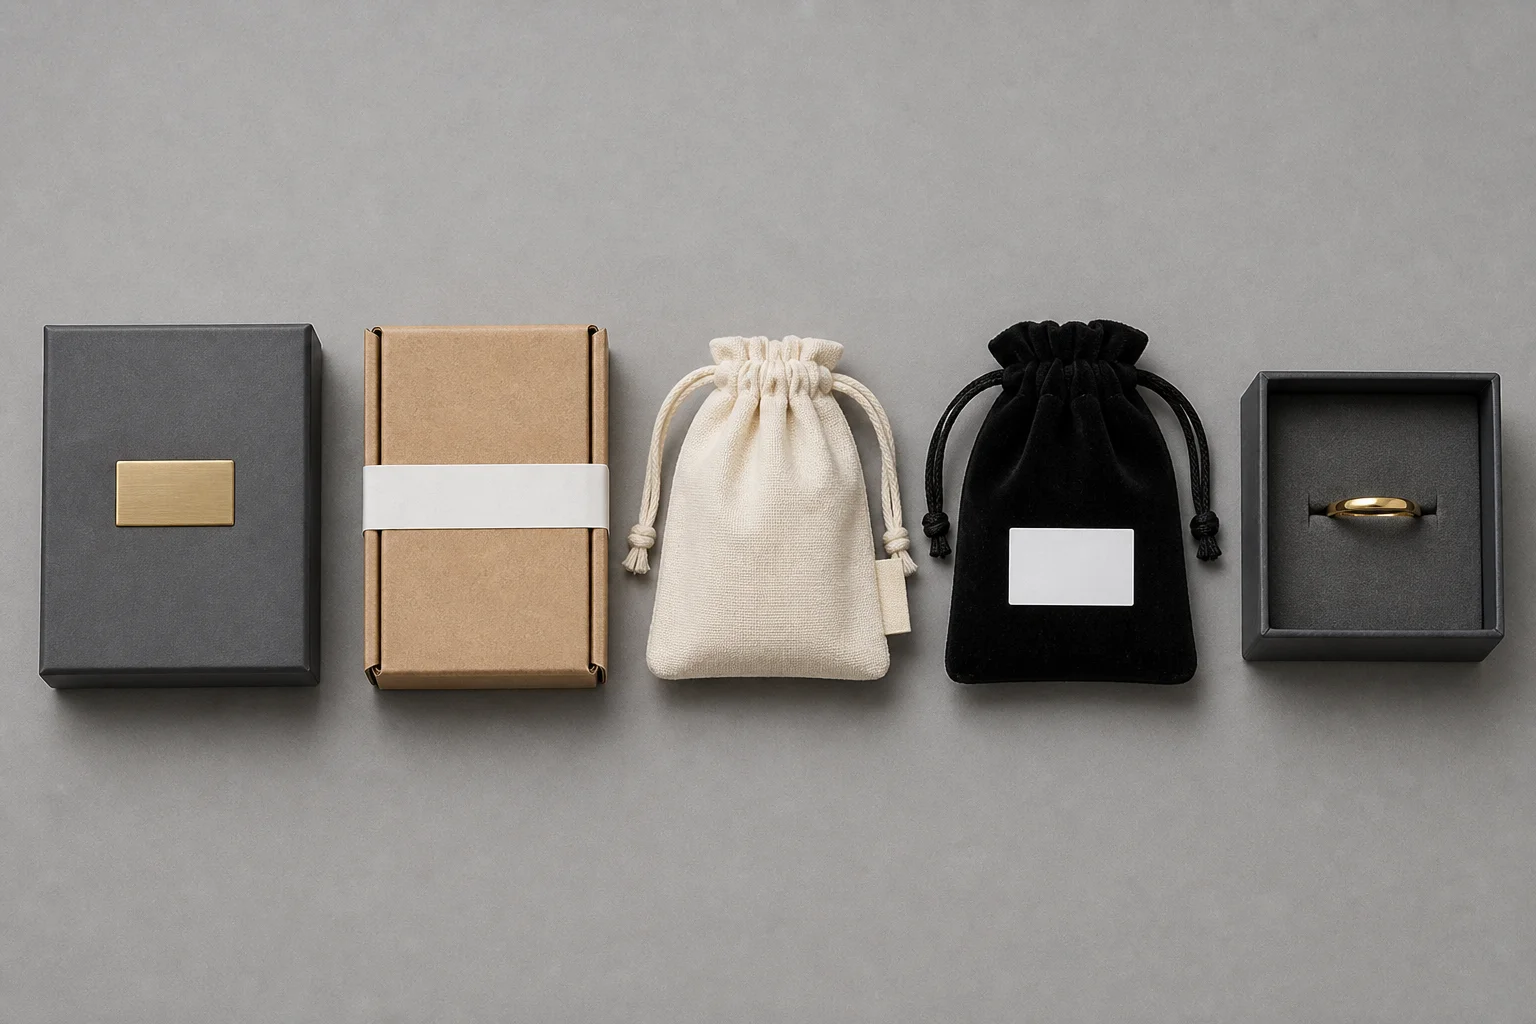
Five applied marks — a brass plate, a paper band, a woven label, an adhesive label and an insert
An applied brand mark is a separate component bonded to a finished pack rather than printed into its surface. The family covers a pressure-sensitive label, a metal or brass plate, a cloth label, a leather patch, a paper tamper seal and an adhesive swing tag. Buying jewelry packaging with logo that way means buying a finished carton plus a second component.
The mark no longer shares a material with the pack. An in-surface mark — foil, embossing, screen print, laser etch — is formed in the board, the wrap or the fabric, so it can only fail by wearing down. An applied mark can fail by coming off, because it was never part of the surface.
That is why the route gets chosen. A custom logo jewelry pouch, a jewelry box with logo applied after wrapping, and most cotton bags with logo are specified for three reasons: no die or colour plate is needed, the mark can vary between lines without retooling, and blank stock can be branded to order — the property a jewelry box private label programme depends on.
Quick Answer: Whether an applied mark stays, lifts cleanly or damages the pack is decided mainly by the substrate's surface strength and by the direction and rate of the force that removes it, not by the strength of the label. Specify the acceptance criterion as fibre tear, name the exact substrate, and state the removal condition the mark must survive.
Adhesive bonding fails in three distinguishable ways. Adhesive failure occurs at the interface, so the mark releases and the pack is undamaged. Cohesive failure occurs inside the adhesive, leaving residue on both faces. Substrate failure occurs inside the board, so the mark takes fibres with it.
Only the third proves the bond is stronger than the material beneath it, and it is the outcome the trade asks for. The accepted rule is that a joint passes when more than half of the affected fibres remain attached to the fractured surface. A mark that releases cleanly has not shown a good bond; it has shown a weak one on a surface strong enough to resist tearing.
In the board study below, the property that most influenced peel adhesion was how the adhesive penetrated the surface; porosity, roughness and contact angle were not significant. A sealed board resists penetration and gives a weak joint; an open board draws the adhesive in, holds harder, and delaminates visibly if the joint is opened.
Brand Background: The evidence here is documented third-party research rather than a single order, and neither study was run on jewelry packaging. One is a paperboard adhesion study by the Pulp and Paper Institute in Ljubljana, published in Applied Sciences in 2023; the other is a peel study from the Department of Chemical Engineering at McMaster University, presented at the 13th Fundamental Research Symposium in Cambridge in 2005.
The Packaging Challenge: Both exist because the trade lacked an objective test. The board study records that no standard method exists for evaluating adhesion on fibre-based folding boxes, and that the conventional field test — peeling a joint by hand and looking at it — depends on the experience of the person looking.
The Procurement Decision: The board study produced three pilot-scale paperboards at 240 g/m², bonded them with a water-based adhesive, and compared a modified T-peel with a Y-peel geometry developed for carton board. The peel study ran pressure-sensitive tape from a library of uncoated papers across a wide range of peel rates, in both machine directions, and used multivariate analysis to separate the adhesive from the paper.
The Solution: Between them the two studies move the question from how strong the mark is to how strong the surface is. One supplies the acceptance rule and the failure vocabulary; the other supplies the variables that change the failure mode without any change to the mark.
Measurable Results: In the board study the sawdust-filled board recorded the highest maximum peel force at 23.8 N in Y-peel against 11.8 N in T-peel, while the same two geometries separated the other boards at 16.9 N against 12.4 N. The board with the highest internal bond strength, 436 kPa in the z-direction, was also the roughest at 3984 mL/min against 1200 mL/min. Penetration dynamics dominated; porosity, roughness and contact angle did not. In the peel study the same tape on the same paper released cleanly at 5 mm/min and delaminated the sheet at 500 mm/min, with a peak force of 408 N/m against a steady state of 208 N/m. Contact angle was not a predictor of adhesion; surface chemistry accounted for 50% of the variation in interfacial peel force.
Mark route | What it needs before production | What can change later | How it fails |
|---|---|---|---|
Foil, emboss, screen print | A die or colour plate, artwork locked at proof | Nothing without a new tool | Wears down, dulls, scuffs |
Pressure-sensitive label | Artwork and a die-cut shape | Wording, colour and even the brand, on blank stock | Lifts at an edge, or tears the board |
Metal or brass plate | A fixture and an adhesive or mechanical fixing | Placement, and the plate itself | Falls away whole, or dents |
Woven or cloth label | Stitching, before the seam is closed | The label, up to that point | Frays, or pulls the seam |
Paper tamper seal | A substrate chosen for its failure mode | The seal graphic | Intended to fail — into the fibre |
Applied routes buy flexibility and pay for it in bond risk; a jewelry box logo formed by foil pays the opposite price.
The substrate sets the ceiling, so it is a decision rather than a background detail.
Substrate | Surface it presents | Expected behaviour in a peel | What the order should state |
|---|---|---|---|
Coated rigid board | Sealed, low-absorption, often wrapped | Adhesive cannot key in, so the mark tends to release | Fibre tear, or a designed clean release |
Uncoated or kraft board | Open, absorbent, visible fibre | The joint outruns the board | A peel that stays on the pack |
Corrugated mailer | Liner surface over a fluted core | Failure can drop into the flute, not the liner | Which ply the mark bonds to |
PU leather wrap | Flexible, elastic, grain-textured | The surface stretches before the joint fails | Load per unit area, not label size |
Velvet-lined board, as on a velvet jewelry pouch with logo | Pile over a backing | The bond forms to the pile, not the structural layer | A pressed or stitched route |
Cotton or muslin cloth | Woven, porous, soft | Adhesive passes through the weave and stiffens the cloth | A sewn woven label, not an adhesive one |
Velvet accepts a mark because the pile grips it, but the pile is not what holds the pouch together; cotton does the opposite, and adhesive sinks into the weave and stiffens it.
One joint fails in different ways depending on how quickly and from which side it is opened — exactly the variation a customer introduces when unwrapping a pack.
Removal condition | What the measurement showed | What it means for a mark |
|---|---|---|
Slow peel, 5 mm/min | Clean interfacial release, no fibre residue | A slow pick at a corner lifts a mark intact |
Fast peel, 500 mm/min | Paper delamination, peak force 408 N/m before steady state at 208 N/m | A quick pull is the condition that proves surface strength |
One machine direction | Repeatable clean release at a higher steady-state force | Direction of pull changes the outcome |
The opposite direction | Repeatable delamination of the sheet | One joint is strong or weak depending which way it opens |
The value that held steady across both directions was the peak force, which is why it is the useful specification figure.
A tamper seal has to leave evidence on the pack, so the joint must be stronger than the outermost layer and no stronger than the layer beneath it.
Seal requirement | Failure mode that delivers it | Substrate implication |
|---|---|---|
Opening must be visible afterwards | Substrate failure, crack running into the fibre | An open surface, not a sealed one |
The pack must not be reusable as new | Substrate failure that cannot be pressed flat | Visible fibre, not a gloss film |
The seal must not fall off in transit | Adhesive and cohesive failure excluded | Pre-press the seal where the joint is loaded |
Line on the order | Why it is required |
|---|---|
Substrate named by grade, not by colour | Surface chemistry and absorption set the achievable bond |
Acceptance stated as fibre tear | Over half the affected fibres must remain on the fractured surface |
Removal direction and rate named | The same joint passes or fails depending how it is opened |
Bonded area and load per unit area | A large label on an elastic wrap behaves unlike a small one |
Whether a clean release is intended | Tamper seals and decorative marks want opposite outcomes |
A custom logo jewelry packaging programme can be audited against those five lines in one production visit. Worked examples of how the same lines change an outcome are collected in the case studies and FAQ on custom packaging sourcing.
What applied marks buy:
A jewelry pouch custom logo order can run on blank stock, so the pack is bought once and branded later.
No print die or colour plate is needed, which keeps entry volume low for a new brand.
One component serves board, cloth and metal packs, so one artwork stays in use.
What they cost:
Adhesion is capped by the substrate, so the pack choice partly decides the mark's life.
A coated or sealed board, the finish most brands want, is the surface that grips worst.
The failure mode depends on how a customer opens the pack, which no factory controls.
Q: Why does a label come off cleanly from one jewelry box and tear another?
A: The boards differ in surface strength, not the labels. A coated board resists penetration and releases the mark; an open board bonds harder than its own fibres hold.
Q: Is a stronger adhesive the answer to a mark that lifts?
A: Usually not on a sealed surface, where the adhesive cannot penetrate far enough. Changing the substrate grade, or pressing a smaller area harder, is more reliable.
Q: How should a pass be judged on an applied mark?
A: By fibre tear. The working rule is that a joint is acceptable when more than half of the affected fibres remain attached to the fractured surface.
Q: What does a logo jewelry packaging order need that a printed one does not?
A: A named substrate grade, the peel direction and rate to be tested, and whether a clean release or a permanent bond is wanted.
Q: Are the studies cited here about packaging?
A: Yes, but not about jewelry packaging. One tested paperboards made for folding boxes and established the fibre-tear acceptance rule; the other measured pressure-sensitive tape peeling from uncoated papers.
An applied mark is an adhesive joint, and the variables that decide its outcome belong to the substrate rather than to the component. Published board testing shows that penetration of the adhesive into the surface outweighs porosity, roughness and contact angle, and that a joint is judged acceptable when the failure stays in the fibres rather than at the interface. Published peel testing shows the same joint releasing cleanly at a slow peel and delaminating the sheet at a fast one, in one machine direction and not the other, with surface chemistry accounting for half the variation in the interfacial force. For jewelry packaging with logo supplied as a separate component, the specification follows from that: name the substrate grade, state fibre tear as the acceptance criterion, define the removal direction and rate, give the bonded area, and say plainly whether the mark is meant to survive or to leave evidence.
Utouch Packaging supplies applied and in-surface branding across rigid boxes, pouches and mailers, specified against these lines — the substrate named by grade, the acceptance written as fibre tear, and the removal condition stated on the order rather than left to the packing line. For wholesale and custom enquiries, visit the Utouch Packaging contact page or reach the export team through Xiamen Yu Touch Imp. & Exp. Co., Ltd.
